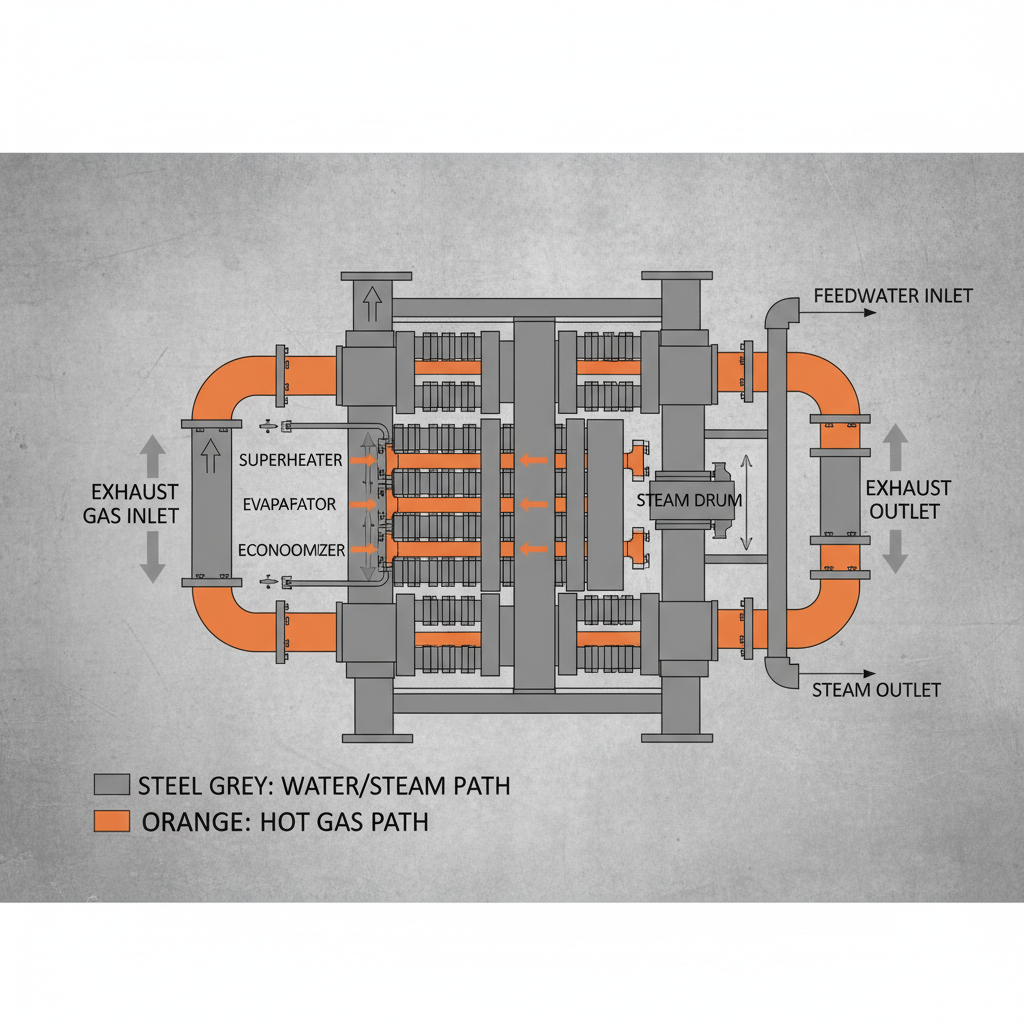
Industrial heating solutions are the backbone of global manufacturing, providing the thermal energy necessary for everything from chemical processing to textile production. Among these, the integration of efficient steam generation and heat recovery systems is critical for maintaining competitive operational costs. A steam boiler with condensor represents a strategic approach to maximizing thermal efficiency by capturing latent heat that would otherwise be wasted.
As global energy prices fluctuate and environmental regulations tighten, the demand for high-performance boiler systems has surged. Industry leaders are no longer looking for simple steam generation; they are seeking integrated systems that reduce fuel consumption and minimize carbon footprints. The adoption of advanced boiler designs ensures that enterprises can scale their production while adhering to strict sustainability benchmarks.
Understanding the technical nuances of these systems is essential for engineers and facility managers. By implementing a steam boiler with condensor, companies can significantly lower their water makeup requirements and enhance the overall lifecycle of their equipment. This guide explores the engineering excellence and practical applications of these systems in modern industrial landscapes.
Advanced Engineering of the DZL Series Boiler
The structural integrity of the DZL series is centered around a specialized drum design featuring arched tube sheets and spirally corrugated tubes. This engineering choice is specifically implemented to prevent tube sheet cracking, a common failure point in high-pressure steam environments. By distributing thermal stress more evenly, the boiler maintains its structural stability over extended operational cycles.
Furthermore, the ascending calandria arrangement under the drum is a critical innovation. This layout eliminates the "dead water zone" typically found at the bottom of the drum, ensuring that sludge cannot easily subside. Consequently, the high-temperature region of the drum receives superior cooling, effectively eliminating the bulge phenomenon and extending the service life of the steam boiler with condensor system.
Thermal Efficiency and Heat Transfer Optimization
The efficiency of a steam system depends heavily on the rate of heat transfer from the combustion chamber to the water. In the DZL series, the use of spirally corrugated tubes serves a dual purpose: it increases the effective heating surface area and creates turbulence in the water flow. This turbulence disrupts the boundary layer, which significantly strengthens heat transfer and allows the boiler to reach rated steam temperatures more rapidly.
Beyond the tubing, the wind box is designed with high-precision sealing to provide a rational and consistent flow of air to the furnace. By optimizing the air distribution, the system reduces the air excess coefficient, which prevents the cooling of combustion gases and ensures that more energy is captured by the water tubes rather than being lost through the stack.
When integrated as a steam boiler with condensor, the system focuses on capturing every possible BTU. The combination of corrugated tubes and an optimized air-to-fuel ratio results in a design efficiency that reaches up to 80.4% in larger models, ensuring that fuel costs are kept to an absolute minimum while steam output remains consistent.
Combustion Dynamics and Emission Control
Effective combustion is the foundation of any high-performance steam boiler. The DZL series employs a rational arch design inside the furnace, which is engineered to improve the overall combustion condition. This design facilitates a more complete burn of the fuel, whether it be coal or biomass, reducing the amount of unburnt carbon leaving the system.
A key advantage of this internal architecture is the enhancement of the dust falling function. By encouraging particulates to fall back into the combustion zone rather than exiting with the flue gas, the steam boiler with condensor significantly reduces pollutant emissions, helping facilities meet stringent environmental air quality standards.
The synergy between the combustion chamber and the exhaust system ensures that smoke emission temperatures are kept within an optimal range (typically between 153.5°C and 167.5°C). This precision in temperature management prevents excessive heat loss and reduces the thermal stress on the exhaust components, ensuring long-term reliability.
Performance Analysis Across Capacity Ranges
The DZL series offers a wide spectrum of capacities, ranging from 1 t/h to 20 t/h, allowing industries to select a system that precisely matches their load requirements. As the capacity increases from the DZL1 to the DZL20, the heating area expands proportionally from 30.5 ㎡ to 712.1 ㎡. This scalability ensures that the boiler operates at its peak efficiency point regardless of the plant size.
Comparing these models reveals that the larger units often achieve slightly higher design efficiencies due to better thermal mass and optimized flow dynamics. For instance, the 15 t/h model reaches a peak efficiency of 80.4%, demonstrating that the steam boiler with condensor architecture becomes even more effective as the scale of operation increases.
Efficiency Comparison for Steam Boiler with Condensor Models
Global Industrial Applications and Use Cases
The versatility of the DZL series makes it an ideal choice for a variety of industrial sectors globally. In the textile and garment industry, these boilers provide the consistent steam required for dyeing and finishing processes. The ability to handle different fuel types, including biomass, allows factories in Southeast Asia and South America to leverage local agricultural waste, significantly reducing their reliance on imported fuels.
In the food and beverage sector, the precision of the steam boiler with condensor is utilized for sterilization, blanching, and evaporation. Because these industries require high hygiene standards and reliable uptime, the elimination of dead water zones and the prevention of tube cracking make the DZL series a dependable asset for ensuring continuous production cycles without unplanned downtime.
Long-term Operational Value and Sustainability
Investing in a high-efficiency boiler is not merely a capital expenditure but a long-term strategy for operational sustainability. The reduction in coal consumption—ranging from 191.5 kg/h for small units to 2980 kg/h for the largest—directly translates into lower procurement costs. Over a ten-year period, the efficiency gains provided by the corrugated tube design can save an enterprise thousands of tons of fuel.
Beyond the financial metrics, there is a significant social and environmental impact. By reducing the air excess coefficient and optimizing the internal furnace arch, these boilers minimize the emission of harmful pollutants. This enables companies to operate in harmony with urban environmental regulations, avoiding costly fines and improving the health of the surrounding community.
Reliability is the ultimate driver of value. The robust construction of the steam boiler with condensor ensures that maintenance intervals are extended. By preventing the bulge phenomenon at the bottom of the boiler, operators spend less time on repairs and more time on production, increasing the overall Return on Investment (ROI).
Technical Specification Comparison and Selection
Selecting the right boiler requires a careful analysis of the rated pressure and steam temperature. The DZL series offers pressures from 0.7 MPa up to 1.25 MPa, catering to different process requirements. For instance, the DZL1-0.7 is perfect for low-pressure heating, while the larger 1.25 MPa models are suited for more demanding industrial steam applications.
Space constraints also play a role in the selection process. With dimensions ranging from 4.6m in length to 8.4m for the largest units, the DZL series is designed to fit into most industrial boiler houses. The modular nature of some units, which are delivered in "top" and "bottom" sections, simplifies the installation process in facilities with restricted access.
Finally, the relationship between the heating area and capacity is the primary indicator of performance. As shown in the technical data, the exponential increase in heating area (up to 712.1 ㎡) ensures that even at maximum capacity, the steam boiler with condensor maintains high steam rates and thermal stability.
Core Technical Parameters of DZL Series Steam Boilers
|
Boiler Model
|
Capacity (t/h)
|
Rated Pressure (MPa)
|
Design Efficiency (%)
|
| DZL1-0.7-AII |
1 |
0.7 |
78.9 |
| DZL2-1.0-AII |
2 |
1.0 |
78.1 |
| DZL4-1.25-AII |
4 |
1.25 |
78.0 |
| DZL10-1.25-AII |
10 |
1.25 |
79.8 |
| DZL15-1.25-AII |
15 |
1.25 |
80.4 |
| DZL20-1.25-AII |
20 |
1.25 |
80.1 |
FAQS
The spirally corrugated tubes increase the internal surface area and induce turbulence in the water flow. This turbulence prevents the formation of a stagnant boundary layer, which significantly enhances the heat transfer coefficient. As a result, the boiler can speed up temperature rises and maintain a higher steam rate compared to traditional smooth-tube boilers.
The ascending calandria arrangement is designed to eliminate "dead water zones" at the bottom of the drum. In standard designs, these zones allow sludge to accumulate, leading to localized overheating and the "bulge phenomenon." By eliminating these zones, the DZL series ensures better cooling of the high-temperature drum region and reduces maintenance needs.
Yes, the DZL series is designed for versatile combustion. The rational arch inside the furnace is optimized to handle various solid fuels, including coal and biomass. The design improves combustion conditions and enhances the dust-falling function, ensuring that biomass can be burned efficiently with reduced pollutant emissions.
A well-sealed wind box provides a rational and uniform distribution of air to the furnace. This prevents "air leaks" and reduces the air excess coefficient. When the air-to-fuel ratio is optimized, the combustion temperature remains high and stable, which increases the overall thermal efficiency of the steam boiler with condensor system.
The smoke emission temperatures for the DZL series typically range from 153.5°C to 167.5°C depending on the model. These temperatures are carefully managed to ensure that maximum heat is extracted from the flue gas while preventing the condensation of corrosive elements in the exhaust stack.
For a 10 t/h requirement, the DZL10-1.25-AII is the ideal choice. It offers a rated pressure of 1.25 MPa, a heating area of 364.6 ㎡, and a design efficiency of 79.8%. This model balances high output with excellent fuel economy and a compact footprint of approximately 6.6m x 2.53m x 1.72m.
Conclusion
The DZL series demonstrates how advanced engineering—such as corrugated tubing, optimized calandria arrangements, and precision combustion arches—can transform a standard industrial boiler into a high-efficiency thermal power plant. By focusing on the elimination of dead zones and the maximization of heat transfer, a steam boiler with condensor provides the reliability and efficiency required by modern manufacturing. From the 1 t/h small-scale units to the 20 t/h heavy-duty systems, the core objective remains the same: reducing fuel consumption while maximizing steam output.
As the industry moves toward a greener future, the ability to utilize biomass and reduce pollutant emissions will become the primary competitive advantage for any facility. We recommend that plant managers conduct a thorough thermal audit to determine the optimal capacity and pressure ratings for their specific needs. Investing in high-efficiency technology today ensures a sustainable, cost-effective, and compliant operation for decades to come. Visit our website for more information: www.ynboilers.com