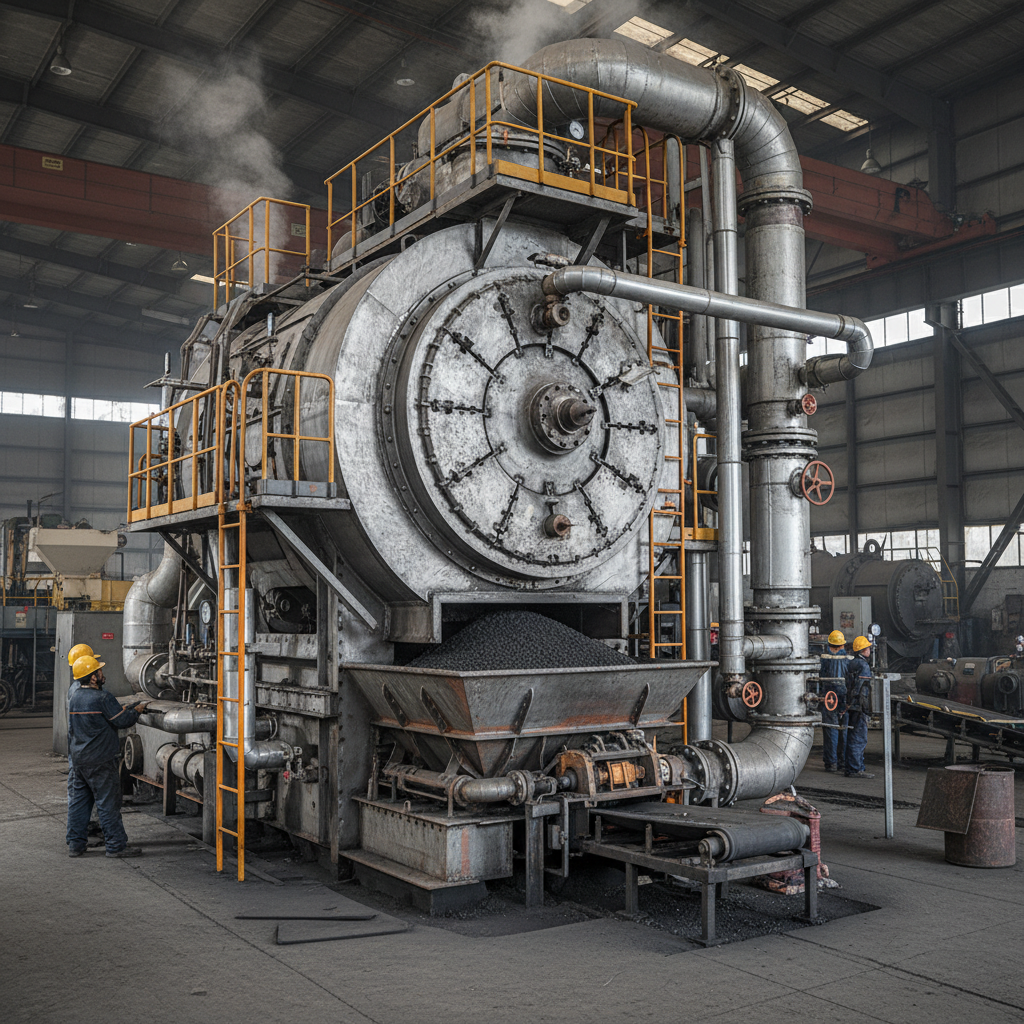
In the modern industrial landscape, thermal efficiency is not just a technical preference but a financial and environmental necessity. A steam boiler economizer represents a critical advancement in heat recovery, designed to capture waste heat from flue gases and repurpose it to preheat feed water, thereby reducing the fuel consumption required to reach boiling point.
Globally, the push toward decarbonization and the volatility of fuel prices have forced manufacturers to look closer at their energy losses. By integrating sophisticated heat exchange mechanisms, industries can significantly lower their operational overhead while adhering to stricter ISO environmental standards and reducing their overall carbon footprint.
Understanding the mechanics and strategic implementation of a steam boiler economizer allows plant managers to transform energy waste into a competitive advantage, ensuring that every calorie of heat is utilized to its maximum potential.
Advanced Structural Integrity of Heat Recovery Systems
The reliability of a heat recovery system depends entirely on the quality of its fabrication. To ensure maximum longevity, the heating surfaces are fully fused using argon-shielded welding, a process that minimizes oxidation and ensures a leak-proof seal. Every critical joint undergoes rigorous X-ray inspection and water pressure testing to guarantee that the system can withstand the intense thermal stresses associated with industrial operations.
Beyond welding, the integration of patented top coil technology significantly enhances the system's lifespan. By heating the furnace tubes on both sides and extending the residence time of high-temperature flue gases, the design prevents premature wear and optimizes the thermal exchange process, ensuring that the equipment remains operational under heavy loads without frequent maintenance.
Thermal Efficiency and Biomass Fuel Versatility
One of the most significant challenges in boiler operation is the inconsistent quality of biomass fuels. To address this, a uniquely designed special furnace arch is employed, which allows the system to burn various biomass fuels effectively. This versatility ensures that users can switch fuel sources based on availability and cost without sacrificing the overall combustion quality or the stability of the heat output.
Efficiency is further bolstered by the strategic arrangement of the internal components. By prolonging the contact between the hot gases and the heat exchange surfaces, the system captures energy that would otherwise be lost through the stack. This approach allows the boiler to achieve efficiency ratings reaching up to 79.1% depending on the capacity, marking a substantial improvement over traditional non-economized systems.
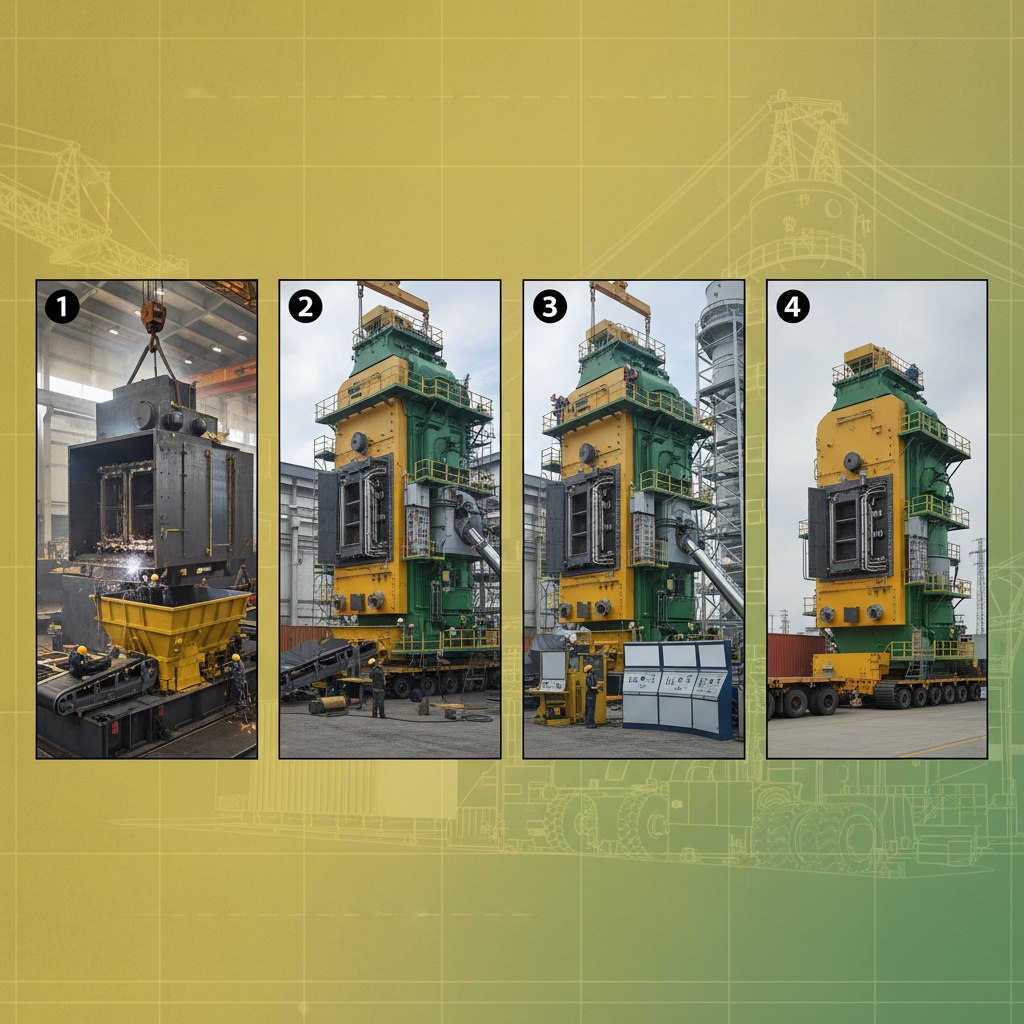
Furthermore, the focus on "factory-complete" assembly reduces the risk of on-site installation errors. By completing the assembly and fixing of internal system piping within a controlled factory environment, the end-user receives a product that is ready for direct connection, minimizing construction downtime and ensuring that the thermal performance is exactly as specified in the technical parameters.
Defining the Modern Steam Boiler Economizer
In simplest terms, a steam boiler economizer is a heat exchanger that recovers heat from the boiler's exhaust gases to preheat the feed water before it enters the steam drum. This process reduces the amount of fuel needed to convert water into steam, creating a more sustainable loop of energy usage within the plant.
The implementation of a steam boiler economizer is especially critical in industries where water heating costs represent a large portion of operational expenses. By leveraging the latent heat of flue gases, the system effectively lowers the "thermal shock" to the boiler shell, which in turn reduces mechanical stress and extends the equipment's total service life.
Beyond the technicalities, this technology addresses the humanitarian and global need for reduced emissions. As industries shift toward biomass and greener energy sources, the efficiency provided by a steam boiler economizer ensures that fewer natural resources are consumed to produce the same amount of industrial steam.
Performance Metrics across Capacity Scales
The performance of these systems scales logically with their capacity, from smaller 240 kW units to massive 2000 kW installations. As the capacity increases, the heating surface area expands—from 17㎡ to 98㎡—allowing for a larger volume of heat exchange. This scalability ensures that whether a facility is a small workshop or a large-scale industrial plant, the energy recovery remains optimized.
Crucially, as the capacity grows, the system's efficiency generally trends upward, reflecting the better heat-to-mass ratio of larger units. This makes the investment in higher-capacity systems not only a matter of output but a matter of superior fuel economy per unit of energy produced.
Comparative Efficiency Rating of Heat Recovery Systems
Global Industrial Applications and Use Cases
These heat recovery systems are deployed across a vast array of sectors, from textile manufacturing in Southeast Asia to food processing plants in Europe. In regions where biomass is abundant, such as agricultural hubs in Brazil or India, the ability to utilize a steam boiler economizer allows factories to leverage local organic waste, turning a disposal problem into a heating solution.
In remote industrial zones where fuel logistics are challenging, the high cost-performance ratio of these boilers becomes a lifeline. By reducing the total volume of fuel required for operation, companies can reduce the frequency of fuel deliveries, thereby lowering transportation costs and reducing the risk of operational downtime due to supply chain disruptions.
Long-Term Value and Sustainability Impact
The long-term value of integrating an economizer extends beyond simple fuel savings. It is an investment in operational stability. By reducing the temperature differential between the feed water and the boiler water, the system minimizes the risk of thermal fatigue in the boiler metal. This results in fewer unplanned shutdowns and a significantly lower total cost of ownership over a 10-to-20-year lifecycle.
From a sustainability perspective, every percentage point increase in efficiency translates directly into fewer tons of CO2 emitted into the atmosphere. For companies pursuing "Green Factory" certifications, the documented efficiency of these systems provides the empirical data needed to prove their commitment to environmental stewardship.
Ultimately, the trust placed in these systems stems from their blend of innovative engineering—like argon welding and X-ray validation—and practical application. It is a logical approach to energy management that balances the need for high industrial output with the ethical requirement for resource conservation.
Technical Specifications and Implementation Analysis
Implementing a heat recovery system requires a precise match between the boiler's capacity and the facility's thermal demand. For instance, a system with a 1000 kW capacity requires a heating surface of 60㎡ and an oil circulation volume of 80 m3/h to maintain optimal efficiency. This technical precision ensures that the heat exchange occurs at a rate that matches the steam production without causing turbulence or pressure drops in the feed system.
The physical dimensions also play a role in installation planning. A 2000 kW system, for example, reaches a height of 6090mm and a weight of 12690kg. Because these are often manufactured as complete units at the factory, the site preparation focuses primarily on the foundation and the direct connection of hot equipment pipelines, which drastically reduces construction time.
When analyzing the cost-performance ratio, the initial investment is offset by the reduced fuel bill and the extended boiler life. The following table provides a comparative breakdown of the technical parameters across different capacity levels to assist in selection.
Technical Parameter Analysis for Various Capacity Models
| Capacity (kW) |
Efficiency (%) |
Heating Surface (㎡) |
Weight (kg) |
| 240 |
74.2 |
17 |
1962 |
| 500 |
74.9 |
32 |
3801 |
| 1000 |
77.5 |
60 |
6043 |
| 1400 |
77.4 |
84 |
8802 |
| 2000 |
79.1 |
98 |
12690 |
| Custom |
Variable |
Custom |
Custom |
FAQS
It works by capturing waste heat from the exhaust flue gases, which would otherwise escape into the atmosphere. This recovered heat is used to preheat the feed water entering the boiler. Because the water is already at a higher temperature, the boiler requires significantly less fuel to raise that water to its boiling point, directly lowering monthly energy expenditure.
Yes, thanks to a specially designed furnace arch and a robust heating surface fused with argon-shielded welding. The design is specifically engineered to manage the combustion characteristics of various biomass sources, ensuring a stable burn and protecting the internal tubes from the corrosive or abrasive nature of certain biomass ashes.
Factory assembly allows for higher precision and quality control. Critical tasks like X-ray inspection of welds and water pressure testing are performed in a controlled environment. This means the equipment arrives on-site as a complete unit, reducing installation time from weeks to days and eliminating the risk of on-site welding defects.
The patented top coil technology ensures that the furnace tube is heated on both sides and increases the residence time of high-temperature gases. By distributing the thermal load more evenly and preventing "hot spots" in the furnace, it reduces the rate of metal fatigue and oxidation, effectively extending the overall operational lifespan of the boiler.
While integrating into an existing system requires careful engineering, our units are designed for ease of connection. Since the internal piping is pre-fixed in the factory, the on-site work is primarily focused on connecting the hot equipment pipelines, making the transition smoother than traditional custom-built on-site installations.
For medium-sized facilities, the 1000kW to 1400kW models are often ideal. These offer a strong balance of efficiency (77.4% - 77.5%) and heating surface area (60-84㎡), providing substantial energy recovery without requiring the massive footprint of the 2000kW unit.
Conclusion
In summary, the integration of a steam boiler economizer is a strategic imperative for any industrial operation seeking to optimize its thermal efficiency. By combining high-grade argon welding, patented heat-exchange technology, and a versatile design capable of handling biomass fuels, these systems provide a tangible reduction in fuel consumption and a significant extension of equipment lifespan.
As the global industry moves toward a more sustainable and energy-conscious future, the transition to high-efficiency heat recovery will separate the market leaders from the laggards. We recommend that plant managers conduct a thermal audit to determine the ideal capacity for their needs and invest in factory-assembled systems to ensure maximum reliability and minimum downtime. For more information on optimizing your thermal plant, visit our website: www.ynboilers.com