Our Gas and Oil Fired Molten Salt Boiler represents the pinnacle of thermal engineering, specifically designed for high-temperature industrial applications. Utilizing a wet-back internal combustion two-pass structure, this boiler achieves exceptional efficiency and a compact footprint. By integrating micro-positive pressure operation, we have significantly enhanced combustion intensity and eliminated air leakage at the furnace door and flue, ensuring maximum thermal output and operational stability.
Engineered with advanced EDA technology and high-efficiency condensation systems, the boiler optimizes flue gas flow and heat exchange to reduce exhaust temperatures and minimize energy waste. The system is coupled with a world-class PLC automation core from Siemens, providing real-time monitoring of pressure and temperature through a closed-loop PID control system. This ensures a precise, safe, and sustainable heating solution that meets stringent national low-nitrogen emission standards.
Detailed Parameters
| Capacity Range (KW) | 450 - 4700 | Max. Temperature (℃) | 450 |
|---|---|---|---|
| Thermal Output (Kcal/h) | 40 - 400 x10⁴ | Working Pressure (Mpa) | 1.1 |
| Circulating Oil Volume (m³/h) | 18 - 100 | Molten Salt Volume (m³) | 0.61 - 5 |
| Thermal Efficiency (%) | Up to 96.28% | Connecting Pipe (DN) | 65 - 200 |
| Boiler Weight (kg) | 4384 - 16657 | Furnace Surface Temp. | < 50℃ |
Key Advantages
High Thermal Efficiency
Combines wet-back structure and condensation technology to reach efficiencies over 96%.
Advanced EDA Design
Precision calculation of flue gas flow ensures optimal heat exchange and reliable operation.
Low Emission Standard
Innovative combustion design reduces nitrogen oxides to meet strict environmental regulations.
Intelligent PLC Control
Siemens-based automation with PID closed-loop control for stable, real-time parameter management.
Compact Structure
Micro-positive pressure operation allows for a smaller volume without sacrificing capacity.
Premium Components
Equipped with world-renowned imported burners and high-grade refractory insulating materials.
Product Gallery


Management Platforms
Real-time Monitoring
Centralized display of inlet/outlet temperature and pressure in the control cabinet.
PID Closed-Loop
Ensures the boiler operates stably at user-defined temperature setpoints.
Smart Alarm System
Automatic detection and alerts for abnormal temperature rises or operational deviations.
Environmental Compliance
Continuous monitoring of combustion emissions to maintain low-nitrogen standards.
Group Control Support
Expandable control modules allowing for the management of multiple boiler units.
Remote Access
Capable of deep application integration for remote monitoring and operation.
Investment Return Comparison
| Feature | Standard Boilers | Our Molten Salt Boiler |
|---|---|---|
| Thermal Efficiency | 80% - 85% | Up to 96.28% |
| Emission Levels | Standard NOx | Low-Nitrogen Certified |
| Control Precision | Manual/Basic Auto | Siemens PLC PID Control |
| Heat Loss | Higher Surface Temp | Surface Temp < 50℃ |
| Energy ROI | Moderate | High (via Condensation Tech) |
Frequently Asked Questions
Molten salt boilers can operate at significantly higher temperatures (up to 450℃) without the high-pressure risks associated with steam, providing superior heat transfer for specific industrial processes.
By utilizing a new combustion design and high-precision imported burners, the boiler optimizes the fuel-air ratio to minimize the formation of nitrogen oxides during the combustion process.
Yes, our control modules have powerful expansion capabilities, allowing for tailored group control, remote monitoring, and specific PID parameter tuning based on customer requirements.
Condensation technology effectively reduces exhaust gas temperatures and recovers latent heat, which significantly increases thermal efficiency and reduces fuel consumption costs.
We utilize a combination of reasonable structural design and premium-grade refractory and heat-insulating materials to minimize radiation heat loss.
We use imported burners from several well-known international brands, ensuring that the equipment adapts to various fuel qualities and application scenarios while maintaining high safety standards.
Ready to Optimize Your Industrial Thermal Efficiency?
Contact Us-
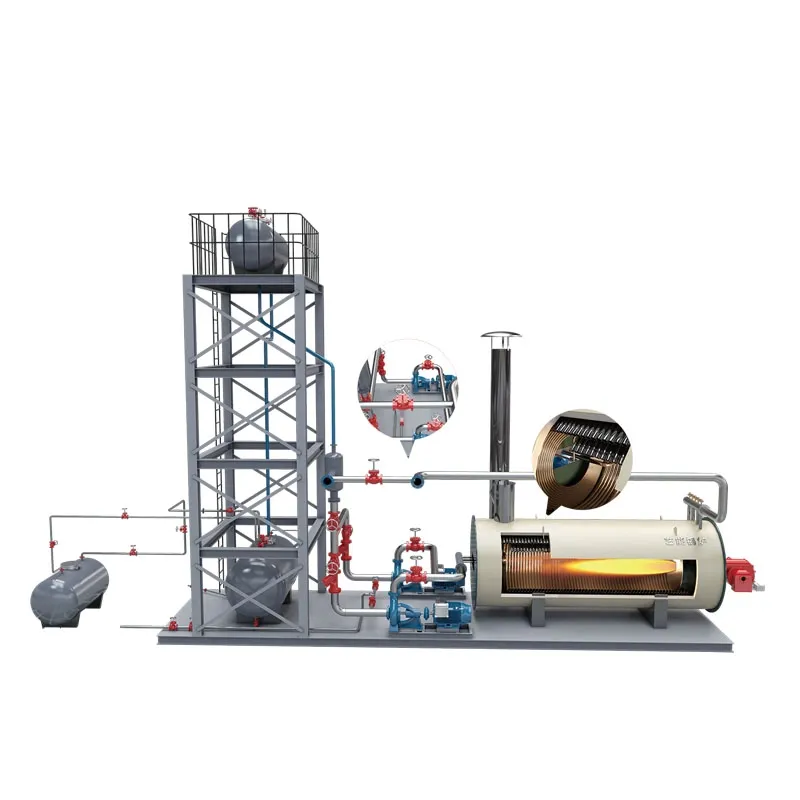
Skid mounted thermal oil boiler
16836
160
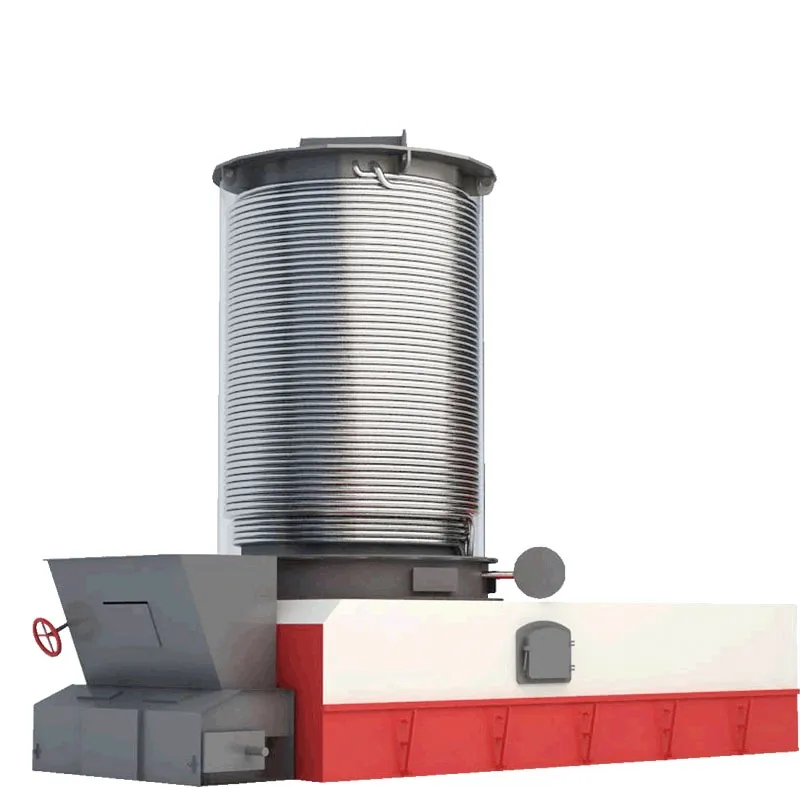
Vertical YLL coal fired chain grate thermal oil boiler
16836
162
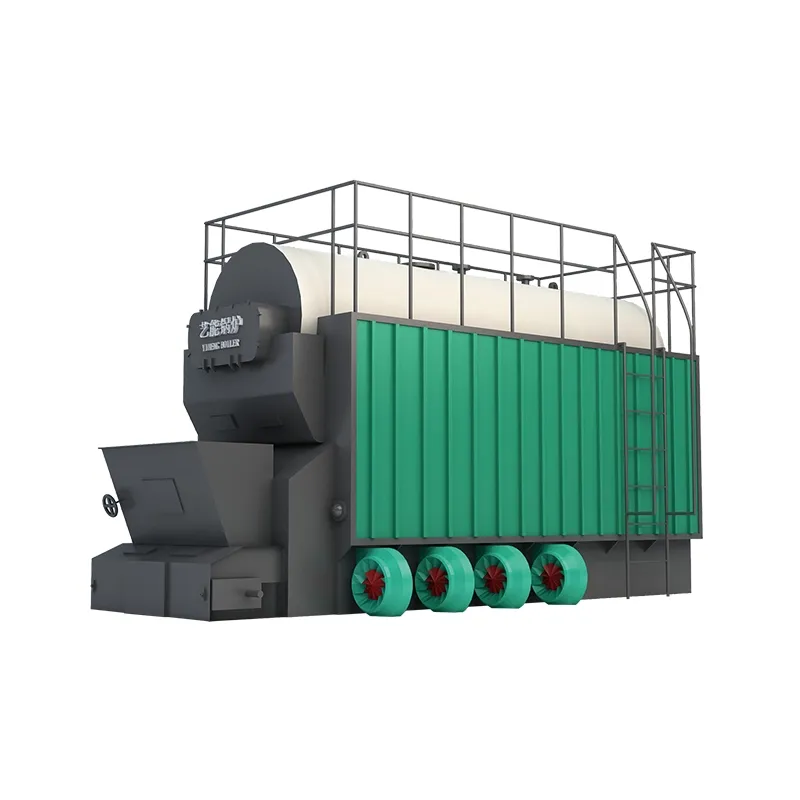
Coal or biomass fired DZL automatic chain grate steam boiler
16836
168
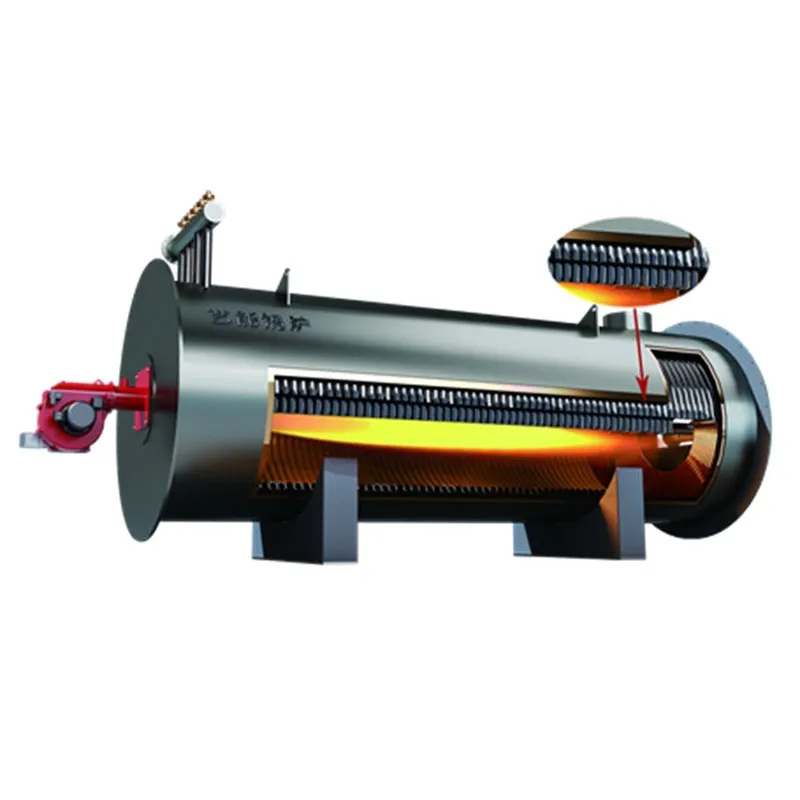
Horizontal YQW gas oil fired thermal oil boiler
16836
158
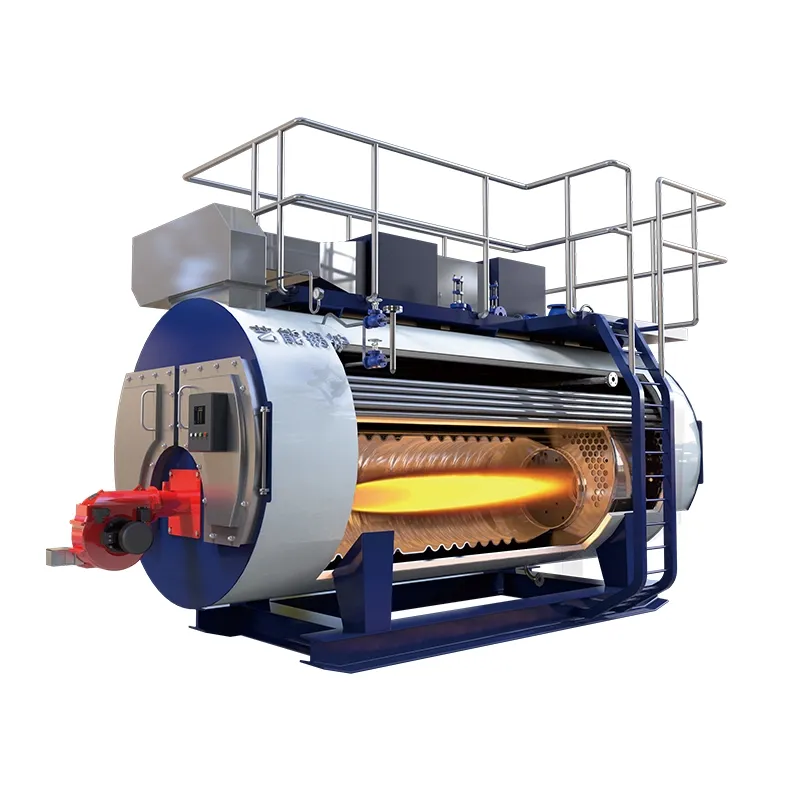
WNS energy saving gas or diesel fired steam boiler
16836
165
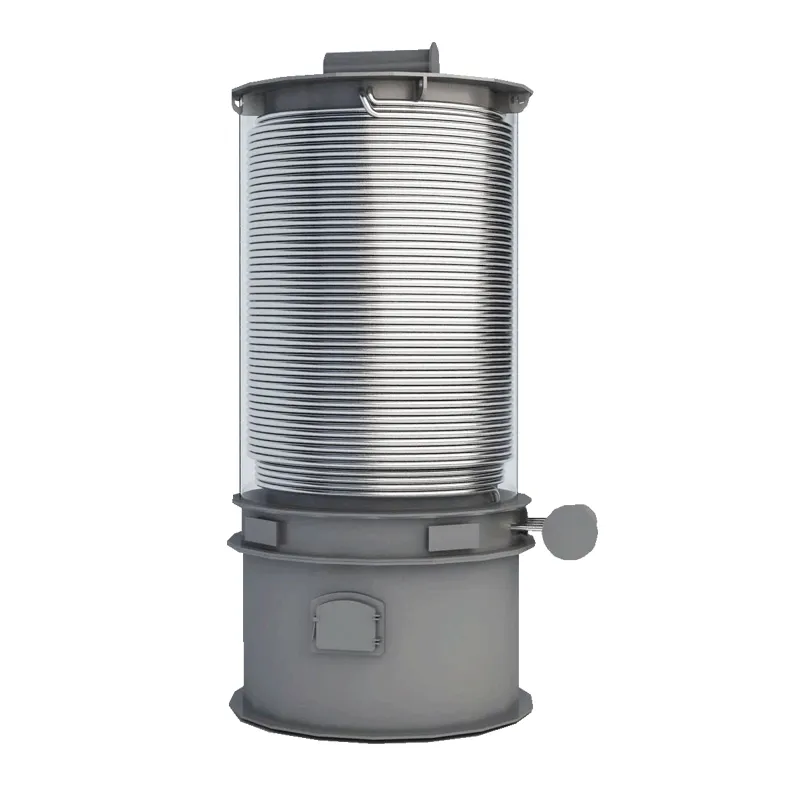
Fixed grate YGL biomass fired thermal oil boiler
16836
163
Electric heating WDR automatic steam boiler
16836
170
Latest News-
 Industrial Energy Efficiency with caldera de recuperación de calor residualMaximizing Energy Efficiency with Caldera de Recuperación de Calor Residual In the modern industrial landscape, energy optimization is no longer optionalit is a competitive necessity. A caldera de recuperación de calor residual waste heat recovery boiler serves as a cornerstone for sustainable manufacturing by capturing thermal energy that would otherwise be lost to the atmosphere. By integrating advanced thermodynamic principles and high-efficiency materials, these systems significantly reduce fuel consumption and carbon emissions. Whether you are operating in the chemical, textile, or food industry, leveraging waste heat allows for a drastic reduction in operational costs while enhancing overall plant productivity.Detail
-
 High Efficiency LSS Industrial Hot Water Heating Boiler GuideOptimizing Industrial Energy with the High-Efficiency Hot Water Heating Boiler In the modern industrial landscape, energy efficiency and reliable thermal management are the cornerstones of operational success. Choosing a high-performance hot water heating boiler is essential for businesses looking to reduce overhead costs while maintaining peak production levels. Whether for climate control, sterilization, or process heating, the right boiler system ensures a steady supply of thermal energy with minimal waste. This guide explores the advanced engineering behind modern through-flow steam and hot water systems, specifically focusing on the LSS series, to help you make an informed investment for your facility.Detail
-
 Best High Efficiency Water Boiler for House and Industrial UseChoosing the Best Water Boiler for House and Industrial Heating Finding an efficient water boiler for house or industrial applications is essential for maintaining consistent thermal energy and operational efficiency. Whether you are managing a residential estate or a specialized manufacturing facility, the quality of your heating system directly impacts energy costs and equipment longevity. Modern boiler technology has evolved to offer high-precision temperature control and environmentally friendly combustion methods. In this guide, we will explore the advanced features of thermal oil and water heating systems, focusing on durability, efficiency, and the technical specifications that set professional-grade boilers apart from standard residential units.Detail
