Our Waste Heat Recovery Boilers are high-efficiency, flue-type heat exchangers engineered to capture and repurpose thermal energy from high-temperature exhaust gases. Specifically designed for heavy industries such as chemical processing, building materials, glass manufacturing, metallurgy, and fertilizer production, these systems prevent energy waste by converting flue gas heat into valuable steam, hot water, or high-temperature heat transfer oil.
By integrating our advanced recovery technology, enterprises can significantly reduce their primary fuel consumption and lower carbon emissions. Our boilers are characterized by a compact structural design and superior heat transfer efficiency, ensuring reliable operation under rigorous industrial conditions. With robust technical support, we provide fully customizable waste heat recovery solutions tailored to your specific thermal load and process requirements.
Detailed Parameters
| Boiler Type | Flue-type Waste Heat Recovery | Heat Carrier | Steam, Hot Water, Thermal Oil |
|---|---|---|---|
| Application Fields | Chemical, Glass, Metallurgy, Fertilizer | Structure Design | Compact & Modular |
| Energy Source | High-Temperature Flue Gas | Heat Recovery Rate | High Efficiency Optimized |
| Operational Mode | Continuous / Process-Linked | Customization | Full Technical Support Available |
| Environmental Impact | Low Emission / Energy Saving | Durability | Industrial Grade Corrosion Resistance |
Key Advantages
Reliable Operation
Engineered for stability in harsh industrial environments, ensuring minimal downtime and consistent thermal output.
Energy Saving
Drastically reduces dependence on external fuel by recycling existing process heat, lowering operational costs.
High Efficiency
Optimized heat exchange surfaces maximize the recovery rate of high-temperature flue gas energy.
Compact Structure
Space-saving design allows for easy integration into existing production lines without extensive remodeling.
Eco-Friendly
Reduces greenhouse gas emissions by optimizing thermal efficiency and decreasing waste heat discharge.
Custom Engineering
Bespoke designs tailored to specific gas compositions and temperature profiles of your industry.
Product Gallery


Management Platforms
Thermal Load Tracking
Real-time monitoring of waste heat input and energy output efficiency.
Automated Control
Intelligent adjustment of flow rates to match fluctuating flue gas temperatures.
Safety Alerts
Instant notifications for pressure anomalies or temperature deviations.
Emission Analytics
Precise data tracking of carbon footprint reduction and energy savings.
Maintenance Scheduling
Predictive alerts for tube cleaning and system inspection intervals.
Remote Diagnosis
Cloud-based technical support for rapid troubleshooting and optimization.
Investment Return Comparison
| Evaluation Metric | Standard Boiler System | Waste Heat Recovery System |
|---|---|---|
| Fuel Consumption | 100% (Baseline) | Reduced by 20% - 40% |
| Operating Cost | High Recurring Cost | Significantly Lowered |
| Carbon Footprint | Standard Industrial Level | Low Emission Profile |
| Energy Efficiency | Moderate | Superior Total Efficiency |
| ROI Period | N/A | Rapid Payback via Savings |
Frequently Asked Questions
They are ideal for any industry producing high-temperature exhaust, including chemical plants, glass factories, metallurgy, fertilizer production, and carbon manufacturing.
Yes, our systems can be customized to generate steam, hot water, or high-temperature heat transfer oil depending on your facility's needs.
By capturing energy that would otherwise be released into the atmosphere, it reduces the need for additional fuel combustion, thereby lowering CO2 and other pollutant emissions.
Absolutely. We offer strong technical support to customize materials and designs to handle specific chemical properties of your exhaust gases.
A compact structure allows for easier installation in existing plants with limited space, reducing the cost of infrastructure modifications.
Our boilers are designed for continuous industrial use with high-grade materials, ensuring reliable, long-term operation with minimal maintenance.
Ready to Optimize Your Energy Efficiency?
Contact Us-
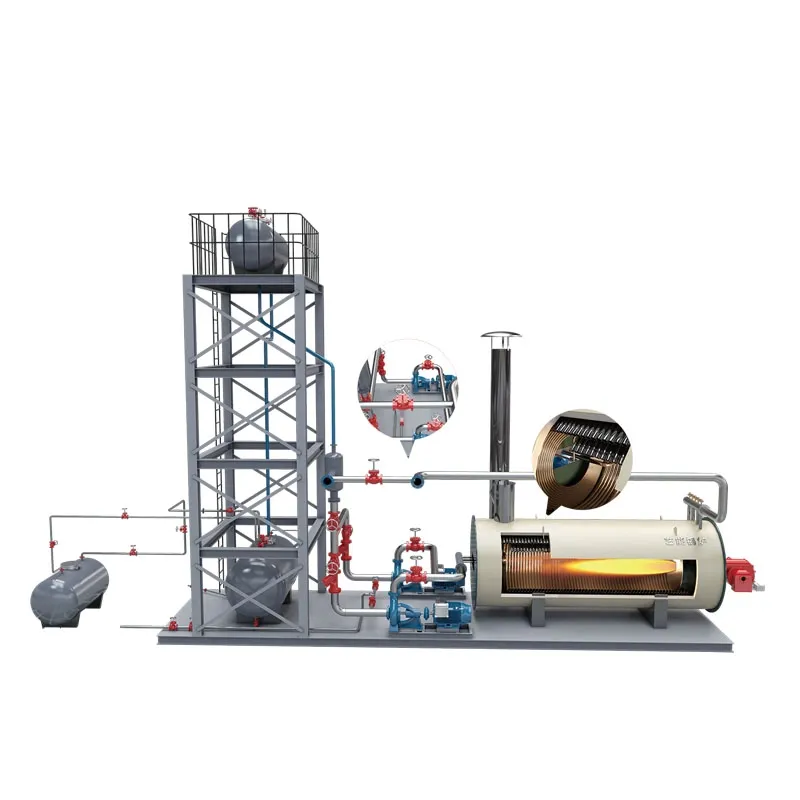
Skid mounted thermal oil boiler
16830
160
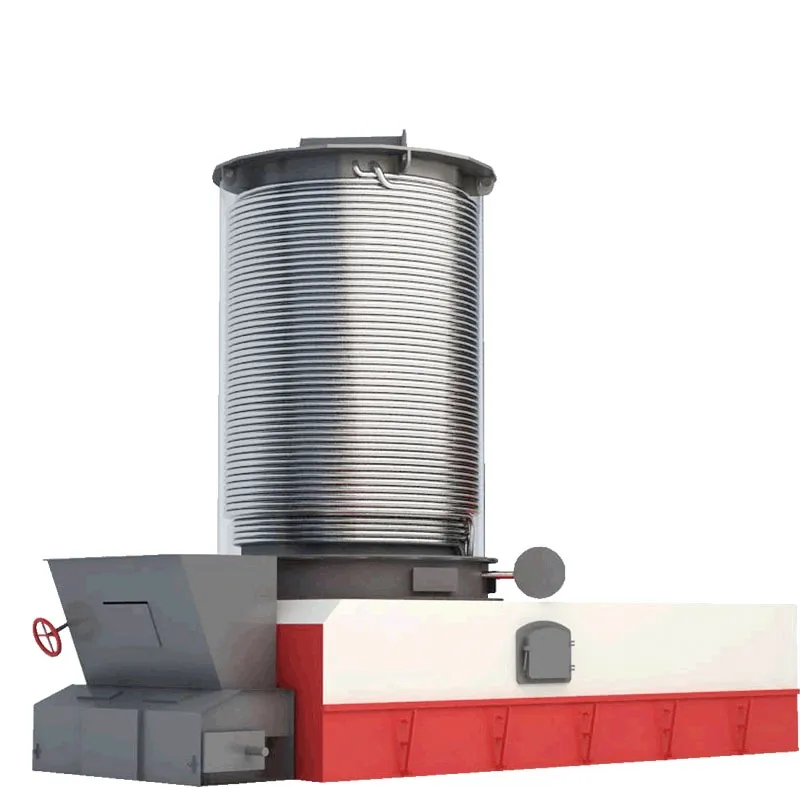
Vertical YLL coal fired chain grate thermal oil boiler
16830
162
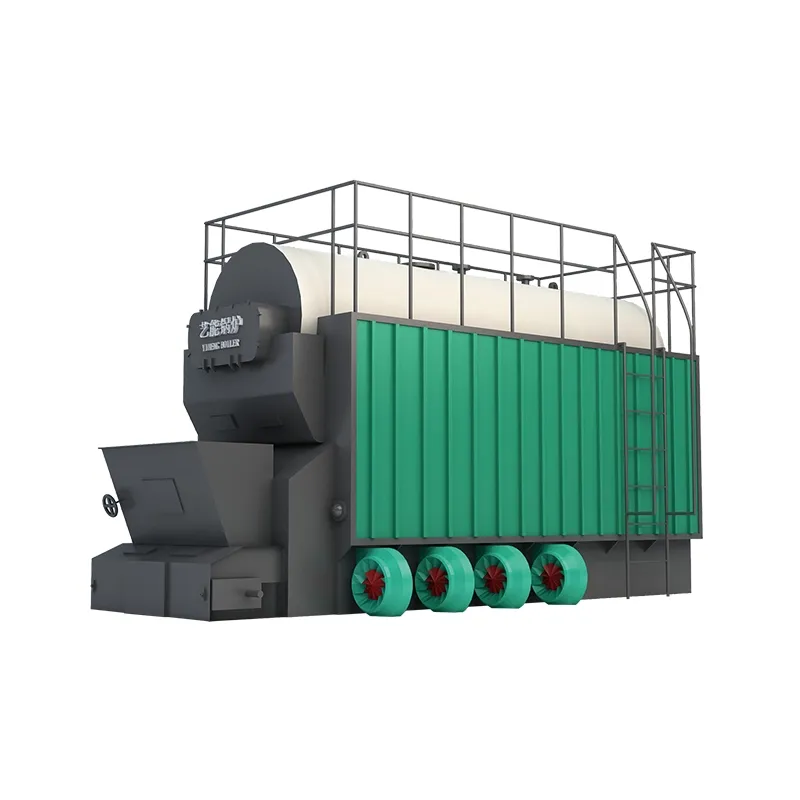
Coal or biomass fired DZL automatic chain grate steam boiler
16830
168
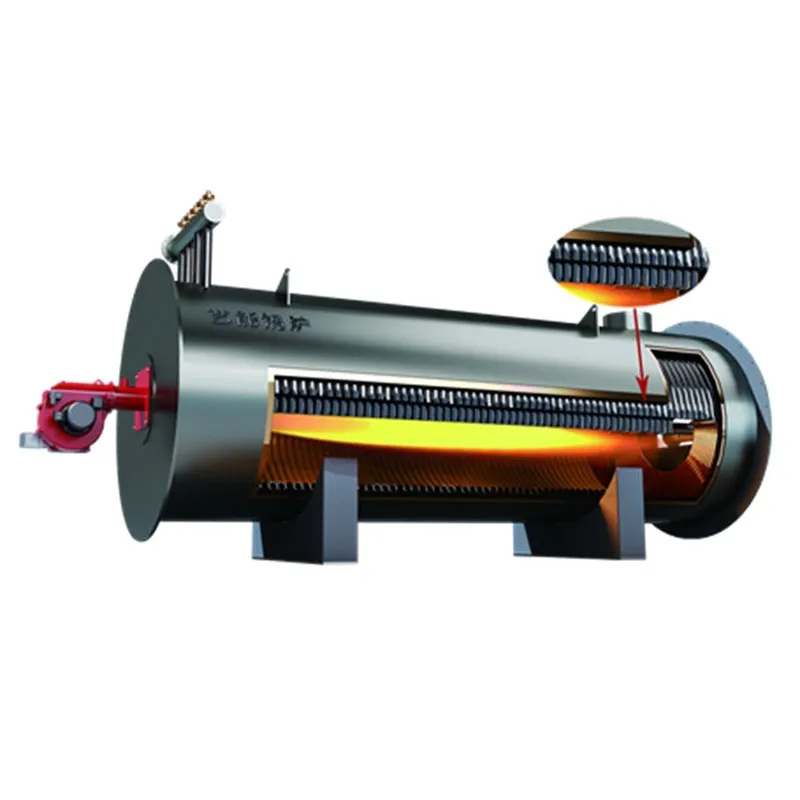
Horizontal YQW gas oil fired thermal oil boiler
16830
158
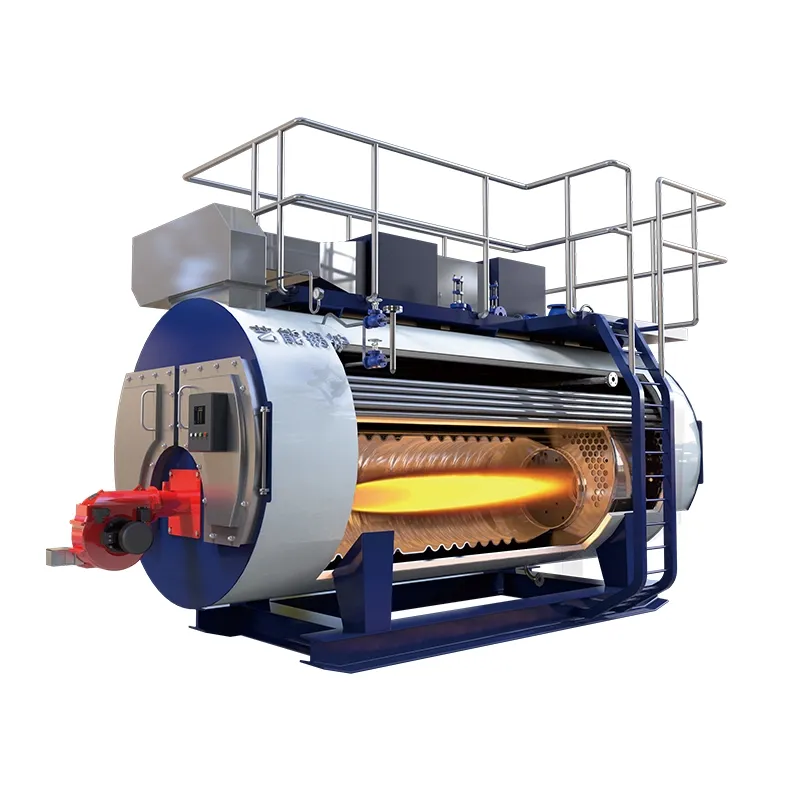
WNS energy saving gas or diesel fired steam boiler
16830
165
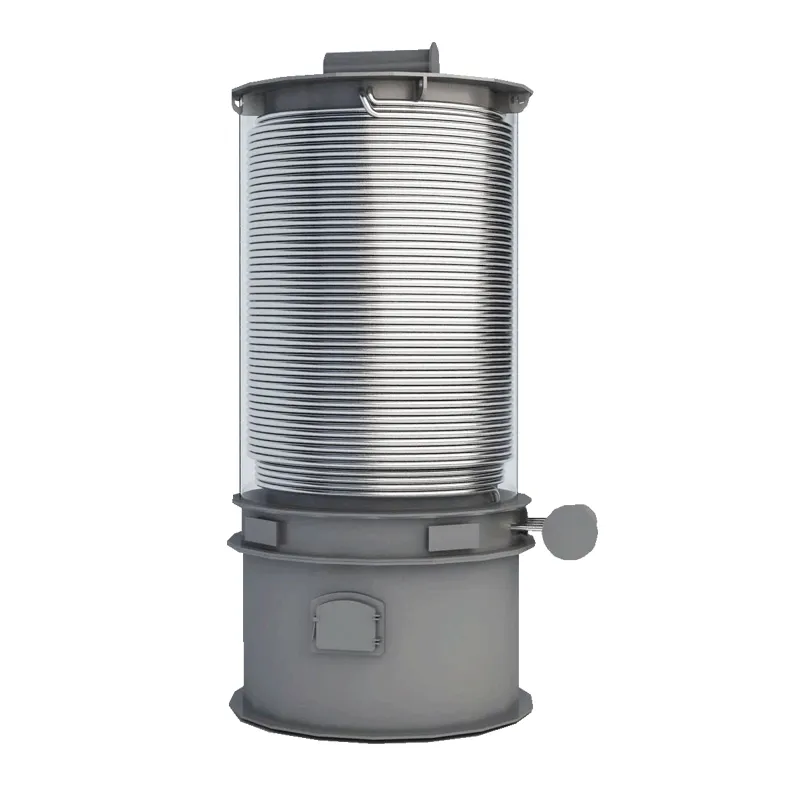
Fixed grate YGL biomass fired thermal oil boiler
16830
163
Electric heating WDR automatic steam boiler
16830
170
Latest News-
 Vertical YLL coal fired chain grate thermal oil boiler vs DZL steam boilerCompare the Vertical YLL coal fired chain grate thermal oil boiler with the DZL steam boiler by pressure, temperature, efficiency, fuel handling, interfaces, and maintenance.Detail
-
 Skid Mounted Thermal Oil Boiler FAQ: Integration, Spare Parts and Maintenance QuestionsCommon questions about skid mounted thermal oil boilers answered — what skid-mounted means, how to integrate the unit on site, what the system includes, and how to plan spare parts and maintenance. Based on Hebei Yineng Boiler Co., Ltd product documentation.Detail
-
 Choosing a Biomass Fired Reciprocating Grate Steam Boiler: Working Requirements and Integration FitLearn the key selection criteria for a biomass fired reciprocating grate steam boiler—fuel compatibility, industrial steam demand, site integration, and sustainability fit—based on confirmed product details from Hebei Yineng Boiler Co., Ltd.Detail
